Frozen Dough Can Fail in Transit Even When the Truck Reads -20°C
Frozen dough and par-baked products often leave the plant intact and arrive damaged, even when the truck log reads -20°C. Small temperature swings in transit grow ice crystals that rupture yeast cells, weaken gluten and loosen crusts. Auditing the route before reformulating can recover quality and margin.
1. Macrotrend and Industrial Reality
Spiral and cryogenic freezers pull the product core below -18°C fast enough to form small, rounded ice crystals that leave the dough structure intact.
Recommended Reading: From our partner FPS Food Process Solutions, where frozen dough quality starts.
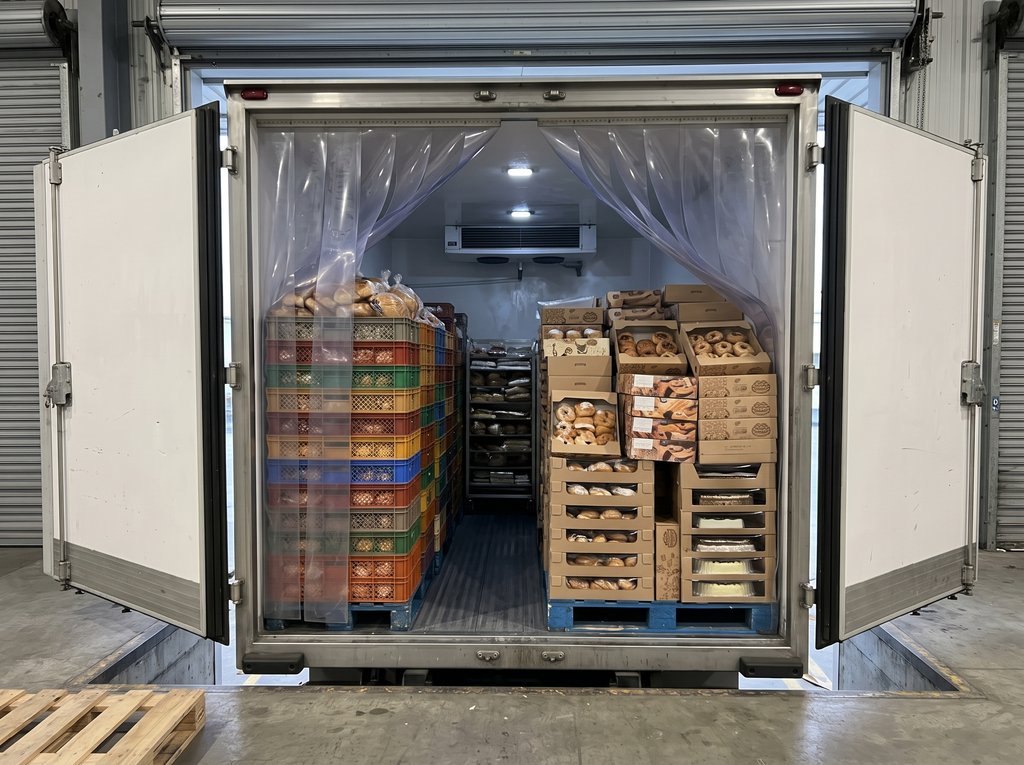
That precision often ends at the loading dock. Control then passes to third-party fleets, cross-docking platforms and multi-drop routes serving supermarkets, convenience stores and foodservice bake-off points.
Frozen dough and par-baked bread are unstable systems. Small temperature swings can damage them while they still look and feel frozen. Close to a third of the water in bread stays unfrozen at -20°C, and the phase surrounding the ice only becomes rigid below roughly -10°C to -15°C. Repeated excursions between -18°C and -12°C are enough to cause irreversible damage.
At the store, the defect tends to be blamed on flour, the bake-off program or the proofer. R&D then reinforces the formula with vital gluten, extra yeast, hydrocolloids and emulsifiers, paying in the mixer for damage that happens on the asphalt.
The “Move to -15°C” initiative proposes raising the frozen setpoint from -18°C to -15°C to cut energy use. For raw dough and par-baked bread, that setpoint leaves almost no buffer; an ordinary deviation in transit places the load in the zone where recrystallization and yeast damage accelerate.
The real stability margin for bakery products sits between the setpoint and the glass transition region of the dough; narrowing it shifts costs onto formulation and customer claims.
2. The Biochemical or Mechanical Challenge
The optical illusion of the trailer
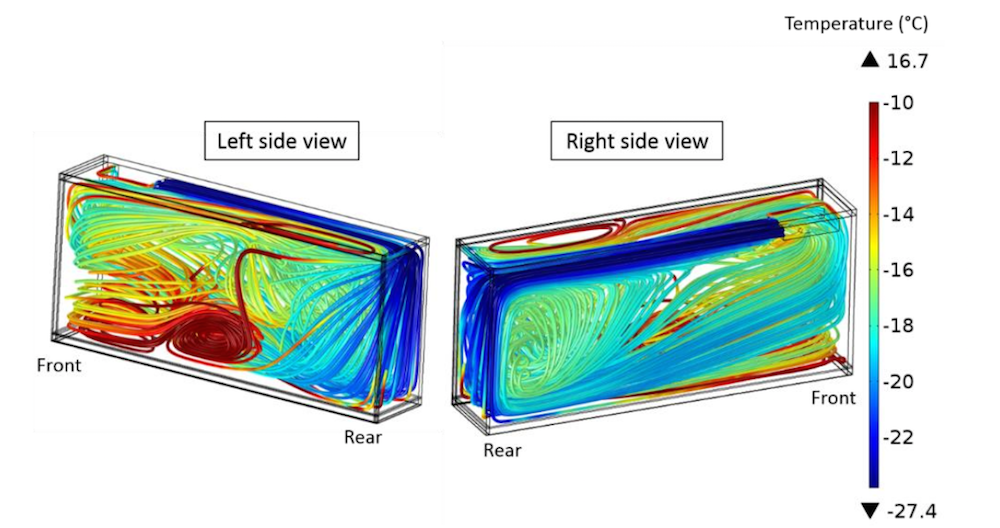
In most front-mounted refrigeration units, the thermostat and cab display read the return air sensor at the front of the box. When airflow is obstructed mid-trailer, supply air hits the first pallets and loops straight back to the return grille.
This short-cycling tells the controller the box has reached setpoint, so the unit throttles down or, in Start/Stop mode, stops the fans. The ticket shows -20°C while pallets near the rear doors and ceiling absorb heat and drift toward -12°C or warmer.
Loading patterns that typically break the air envelope:
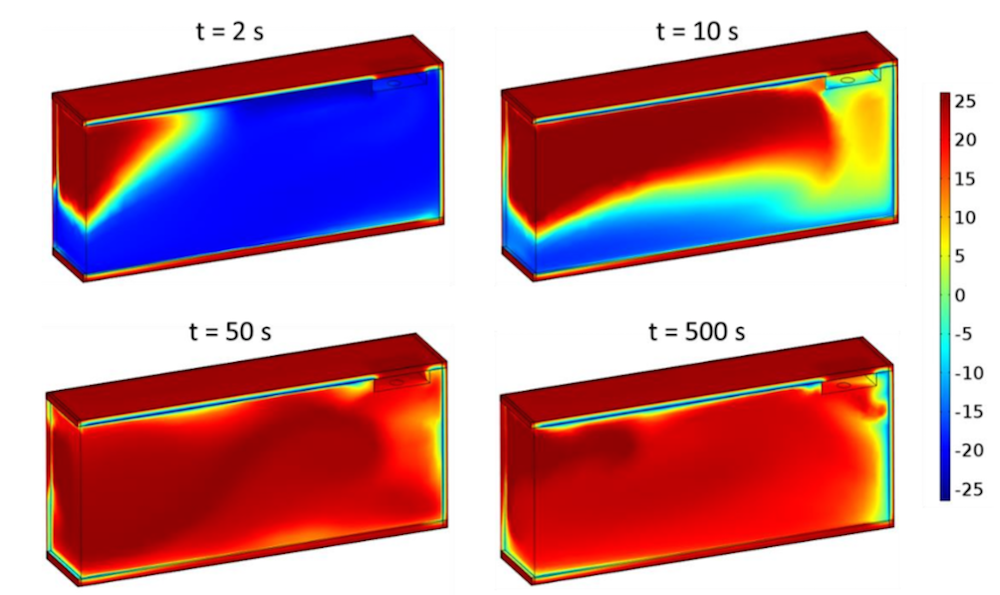
With 25°C outside, warm air floods an open trailer within seconds of opening the rear doors. Running the unit with doors open also frosts the evaporator, often forcing a defrost cycle right after the doors close.
A probe in the pallet center records a flat line, while outer cartons on the same pallet may cycle several times during partial deliveries.
What happens to the dough at -12°C
Each warming episode melts the smallest ice crystals; each cooling episode redeposits that water onto the largest ones. This process leaves fewer, larger and sharper plate-like crystals.
With every cycle, more water leaves the gluten and starch network. In laboratory tests, as few as two freeze-thaw cycles after a month of correct storage markedly increase freezable water and reduce tightly bound water.
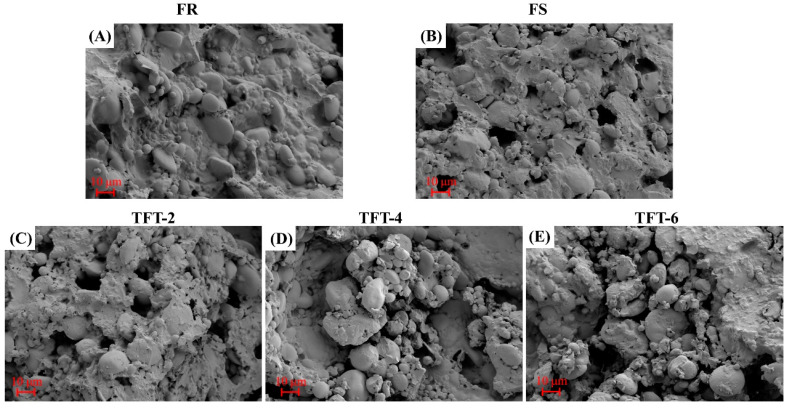
The micrographs below show a harsher version of this process, with full thaws at room temperature. Smooth round granules are starch, the sheet around them is gluten, and dark cavities are pores opened by ice. Fresh dough (A) and dough stored steadily at -20°C (B) keep a continuous gluten sheet; after two, four and six cycles (C to E), pores widen, the gluten loosens and starch granules separate from the network.
In raw frozen dough:
The result typically appears as dough that spreads in the proofer, retains less gas and bakes flat with a dense crumb.
In par-baked bread, starch is already gelatinized and gluten already set, so the weak point is the moisture gap between wet crumb and drier crust.
Above its stability range, surface ice sublimates into the bag headspace and refreezes on the film as loose snow, leaving a pale, dehydrated ring under the crust, known as freezer burn.
Moisture migrating outward freezes just under the crust as a thin ice layer. Crust and crumb contract at different rates, so cycling opens microcracks along that layer. In the bake-off oven, the ice vaporizes and can lift the crust in plates, known as shelling.
Raw dough fails through yeast and gluten chemistry; par-baked bread fails through moisture migration and interface fracture. One route profile can generate two different complaints.
3. Comparative Variables and Technical Parameters
The most useful diagnostic variable is often where damage sits in the shipment. Defects concentrated in top, rear or outer cartons point to transit; defects spread evenly across the lot point to the plant or the store oven.
Misdiagnosis ends up in the formula. The usual reinforcements include:
Excess hydrocolloids compete with gluten for water, raise dough viscosity and tend to reduce machinability, while adding cost and complicating clean label claims.
When symptoms cluster by pallet position, reformulation makes every batch pay for a logistics failure.
4. Solution and Optimization Strategy
The fix starts outside the plant: the truck deserves the same specifications as any other process step. In practice, that means controlling three moments.
Recommended Reading: From our partner EndLine EU, the last step before the truck.
Each control has a price: more fuel, less payload per trip and extra cost per shipment. Climate, route length and number of drops also shape the result.
Once the route holds steady, R&D can remove the extra yeast, gluten and hydrocolloids step by step, checking volume and crust at each stage.
A logger at the rear door may protect margin more effectively than any improver in the recipe.
😊 Thanks for reading!
Sources:
- Dongdong Xie, Xing Li, Jiaxin Zheng: Comparative study on the physicochemical and fermentation properties of dough with three fermentation modes under freeze-thaw cycles / Journal of the Science of Food and Agriculture
- Xiaorong Liu et al.: The Effect of Terminal Freezing and Thawing on the Quality of Frozen Dough: From the View of Water, Starch, and Protein Properties / Foods
- Lin Zhang et al.: Effects of different frozen storage conditions on the functional properties of wheat gluten protein in nonfermented dough / Food Science and Technology
- Ruud van der Sman: Phase field modelling of fracturing in frozen foods / Current Research in Food Science
- Jesus Enrique Gerardo-Rodríguez et al.: Effect of part-baking time, freezing rate and storage time on part-baked bread quality / Food Science and Technology
- Patrick Brecht, Don Durm, Bud Rodowick, Stephen Neel: Refrigerated Transportation Best Practices Guide / IRTA and Global Cold Chain Alliance
- Kuehne+Nagel: Your 5 point guide to mastering reefer container shipping
- Sensitech (Carrier): The Science of Temperature Sensor Location
- Caty Fairclough: Using Simulation to Ensure the Cooling Efficiency of Refrigerated Trucks / COMSOL, SIMTEC and Air Liquide
- Michelle Smith: Hydrocolloids help baked goods manage freeze-thaw cycle / Baking Business
- Lucas Cuni-Mertz: Hydrocolloids are stabilizing superstars in frozen doughs / Baking Business
- Nibedita Das Adhikary et al.: Frozen food packaging: recent technological advances and future perspectives / Frontiers in Sustainable Food Systems
- Nomad Foods: Nomad Foods Achieves Scientific Milestone with Publication of Landmark Frozen Food Storage Study
- Toby Peters, Leyla Sayin: Raising frozen food temperature by 3°C can make global food chain more sustainable, say experts / University of Birmingham
- Stanley P. Cauvain, Linda S. Young: Bakery Food Manufacture and Quality: Water Control and Effects (2nd Ed.) / Wiley-Blackwell
- Stanley P. Cauvain: Frozen Dough and Par-baked Products, in Bakery Products Science and Technology (2nd Ed., ed. Weibiao Zhou et al.) / Wiley-Blackwell
- Stanley P. Cauvain: Baking Problems Solved (2nd Ed.) / Woodhead Publishing
- William P. Edwards: The Science of Bakery Products / RSC Publishing