Multi-Product Bakery Lines Need Cleanable Spiral Freezers
As commercial bakeries diversify their product portfolios, shared production lines routinely handle everything from basic breads to allergen-rich formulations. In this environment, the freezer is no longer simply a piece of thermal equipment. It has become a critical component of a bakery’s sanitation and risk management strategy.
The Reality of Multi-Product Bakery Operations
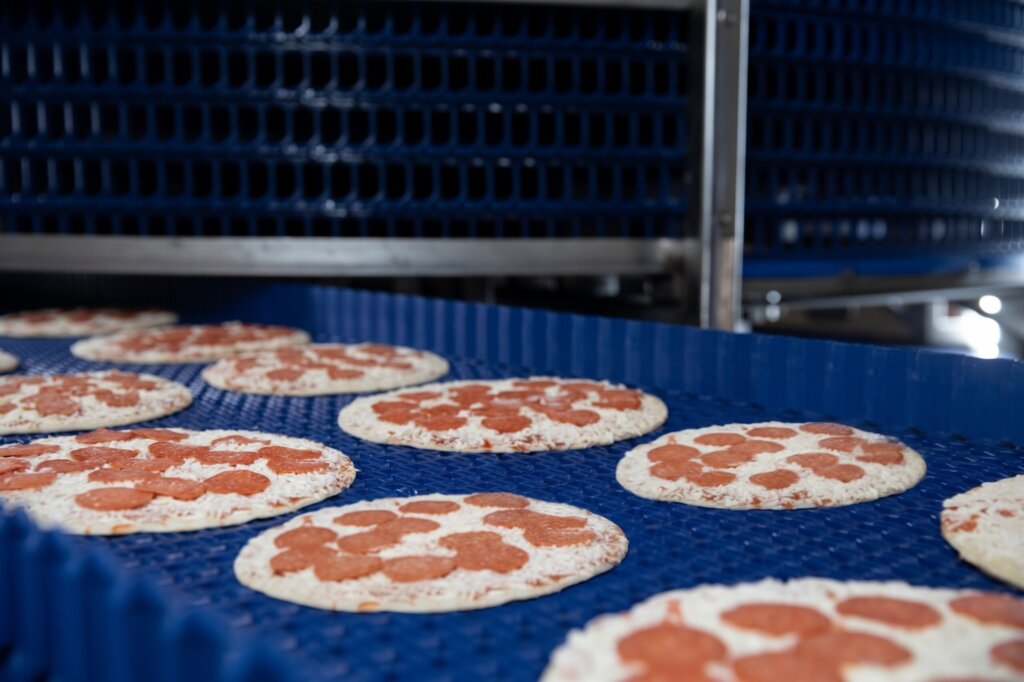
Few bakeries have the luxury of operating dedicated production lines for every product category. The capital investment, floor space, and operational costs required to segregate products are often impractical. As a result, shared production lines routinely process products with varying allergen profiles, ranging from basic formulations to recipes containing soy, dairy, eggs, sesame, nuts, and specialty ingredients.
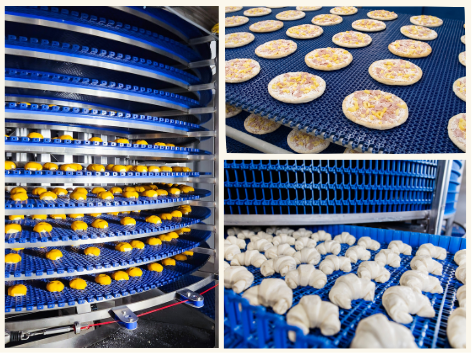
While this approach maximizes production efficiency, it also increases the importance of hygienic equipment design.
Every conveyor, proofer, oven, cooler, and freezer becomes a potential point of cross-contact if not properly cleaned and maintained. Among these systems, spiral freezers present a unique challenge due to their enclosed design, extensive product contact surfaces, continuous airflow, and demanding production schedules.
To manage allergen risks, many bakeries rely on carefully planned production sequencing, running products from the least allergenic to the most complex formulations throughout the week. Once production is complete, a full sanitation cycle is required before returning to non-allergen products. When cleaning procedures are lengthy and labor-intensive, the freezer can quickly become a production bottleneck.
Why Spiral Freezers Can Become a Food Safety Risk
Conventional spiral freezers were historically designed with one primary objective: Freezing Performance.
While effective from a thermal standpoint, many traditional designs were not engineered with sanitation in mind. During operation, high-velocity airflow continuously circulates throughout the freezer chamber.
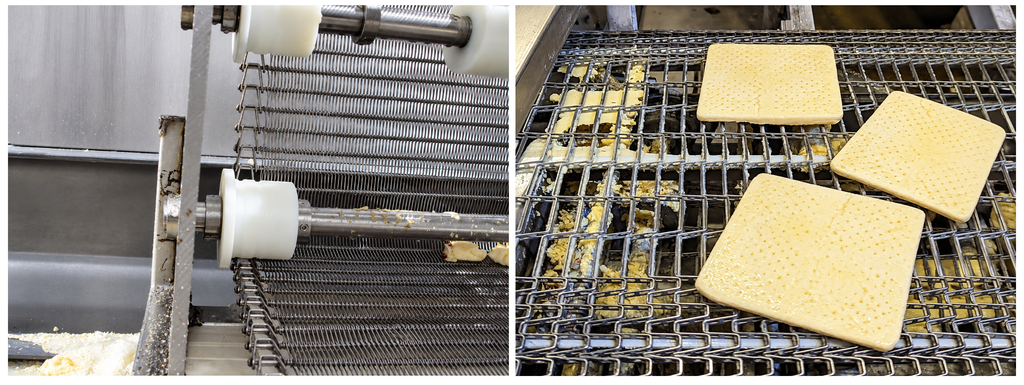
Flour dust, seeds, sugar crystals, dough fragments, and other bakery residues can become airborne and settle on belts, structural components, evaporator coils, drip pans, and other internal surfaces.
Over time, these residues accumulate in areas that can be difficult to access and clean.
Many conventional freezers also contain hollow structural members, bolted connections, overlapping joints, and enclosed mechanical components that can trap moisture and organic material. These conditions increase the risk of allergen buildup and microbial growth, creating potential food safety concerns for facilities processing multiple allergen profiles on shared equipment.
The challenge becomes even greater during changeovers. Before returning to a non-allergen production schedule, processors may need to complete a full defrost, washdown, sanitization, drying cycle, and allergen verification process. In traditional spiral freezer designs, this can result in significant downtime and lost production capacity.
Hygiene by Design
At FPS Food Process Solutions, hygienic engineering is incorporated into the freezer design from the outset rather than being treated as an afterthought.
FPS spiral freezers are constructed from stainless steel 304 materials and feature continuously welded surfaces that eliminate many of the harborage points commonly found in conventional equipment. The design avoids hollow structures, lap joints, and unnecessary surface areas where food particles and moisture can accumulate.
Sloped floors and integrated drainage systems allow wash water to be removed efficiently, eliminating standing water and simplifying sanitation procedures. In addition, drive motors and gearboxes are positioned outside the enclosure, reducing the risk of lubricant contamination while allowing maintenance activities to be completed without entering the freezing chamber.
This hygiene-focused design helps processors achieve more consistent sanitation results while supporting compliance with evolving food safety standards.
Eliminating Mechanical Contamination Risks
Traditional friction-driven spiral freezers present another challenge during extended production runs. As frost and product residue accumulate, friction conditions change, leading to belt slippage, increased wear, and frequent adjustments to maintain reliable operation.
FPS Food Process Solutions addresses this issue with its positive-engagement drive system. Unlike conventional friction drums, the positive-engagement design eliminates belt slippage and overdrive, reducing mechanical wear while improving belt stability and reliability. The result is smoother operation, reduced maintenance requirements, and a cleaner production environment.
Reducing Downtime Through Smarter Defrost and Cleaning Systems
For bakeries, production uptime is just as important as sanitation effectiveness. Every hour spent cleaning is an hour not producing saleable product.
FPS Food Process Solutions helps bakeries maximize operating time through technologies designed to simplify sanitation and extend production campaigns.
Traditional spiral freezers often require frequent production halts simply to clear frost buildup from coils. With FPS Food Process Solutions‘s sequential defrost technology, SynchroSD™, individual evaporator sections are isolated and defrosted one at a time while the remaining sections continue freezing product, keeping the line running without thermal interruptions.
For facilities processing multiple products and allergen profiles, effective cleaning is essential. The FPS Food Process Solutions Recirculating Cleaning System (RCS) provides automated, repeatable washdown cycles that thoroughly clean belts, supports, and other hard-to-reach areas while optimizing water, chemical, and labor usage.
For smaller and mid-sized spiral freezers, the FPS Pressure Cleaning System offers a compact sanitation solution with multi-zone foaming and rinse capabilities that effectively remove flour, gluten, sugars, fats, and other bakery residues.
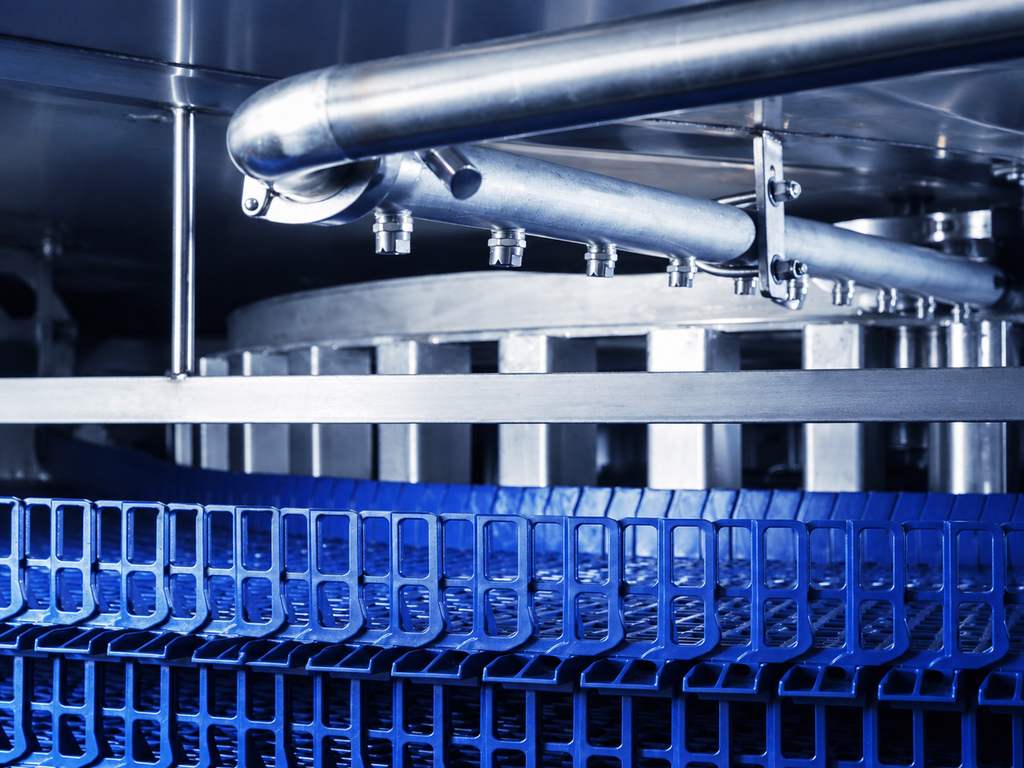
Together, these cleaning systems help bakeries reduce sanitation downtime, improve cleaning consistency, strengthen allergen control programs, and maximize production uptime.
The Bottom Line
As bakeries continue to diversify product offerings while managing increasingly complex allergen programs, cleanability has become just as important as freezing performance. A spiral freezer should not only deliver temperature control and throughput capacity, but also support food safety objectives, simplify sanitation, and minimize downtime.
😊 Thanks for reading!
About The company
FPS Food Process Solutions is a global leader in turn-key food processing solutions, serving customers across six continents. Through its manufacturing facilities, strategic partnerships, and international operations, FPS delivers comprehensive end-to-end processing solutions for food manufacturers worldwide, providing integrated technologies that support efficiency, food safety, and long-term operational success.
Contact:
Global: Suite 110, 13911 Wireless Way, Richmond, BC, Canada V6V 3B9
sales@fpscorp.ca
Europe: Stanleyweg 12, 4462 GN Goes, The Netherlands.
sales@fpseurope.eu
References:
- Spiral Freezers and Chillers, FPS Food Process Solutions. https://www.fpscorp.ca/spiral-freezers
- Bakery Solutions, CMP Equipment (An FPS Company). https://www.cmpequipment.com/bakery
- FPS Bakery Brochure 2025, FPS Food Process Solutions Corp.
- FPS Corporate Introduction 2026, FPS Food Process Solutions Corp.
- Changeover Allergen Cleaning Challenges and Options, AIB International. https://blog.aibinternational.com/en/food-first-blog/postid/134/changeover-allergen-cleaning-challenges-and-options